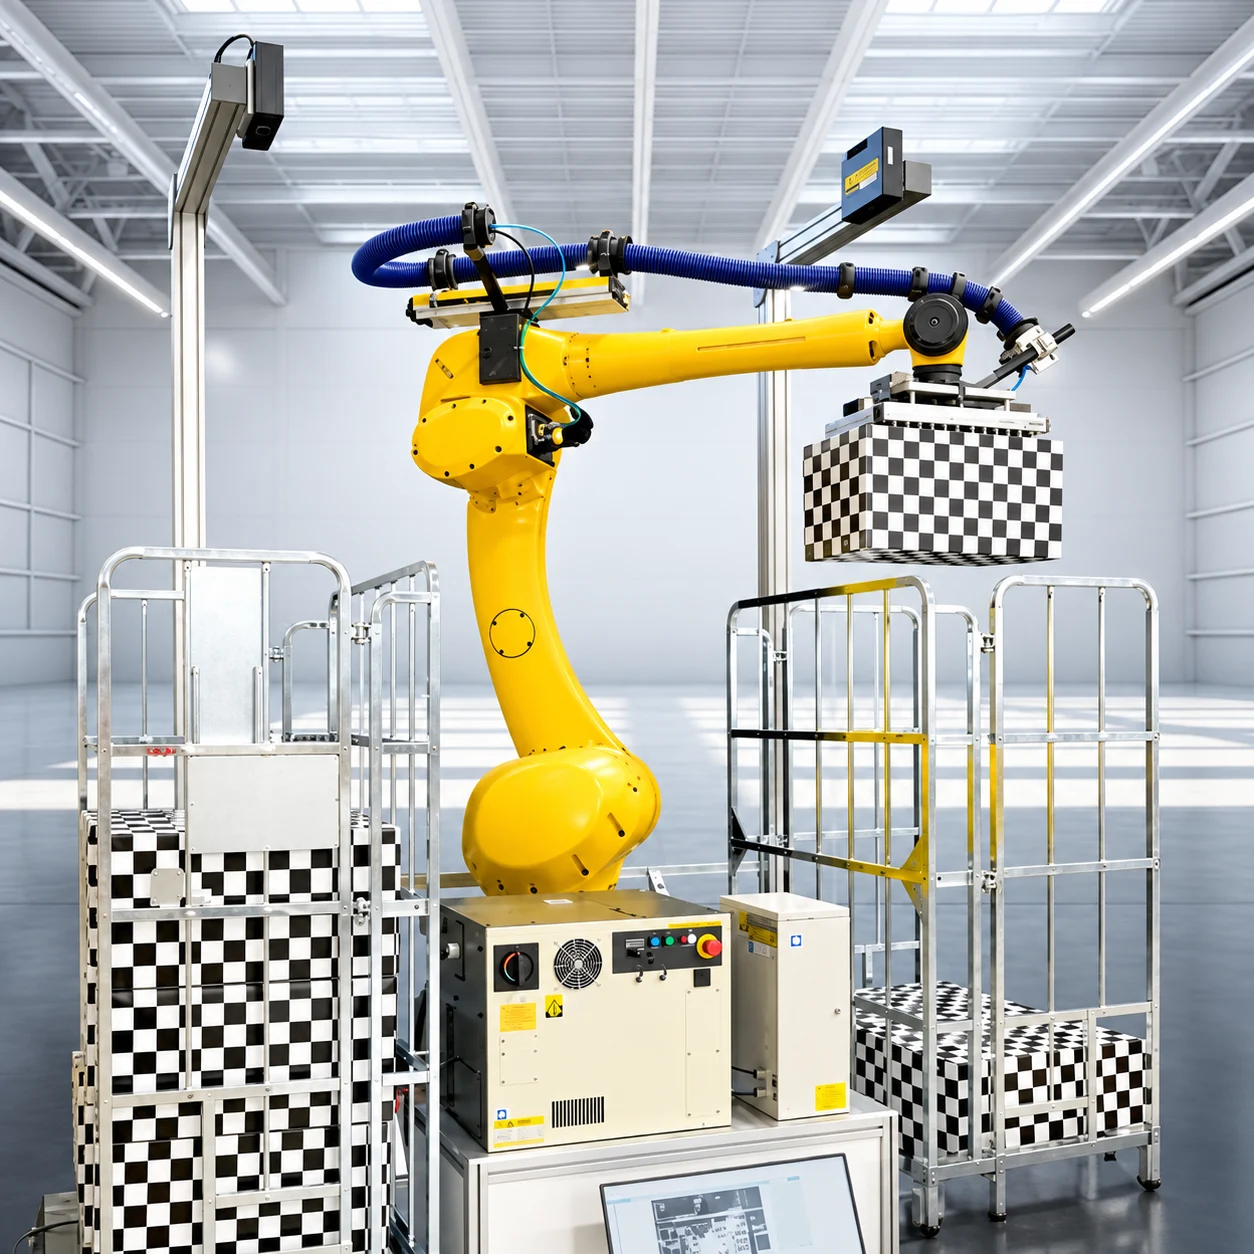
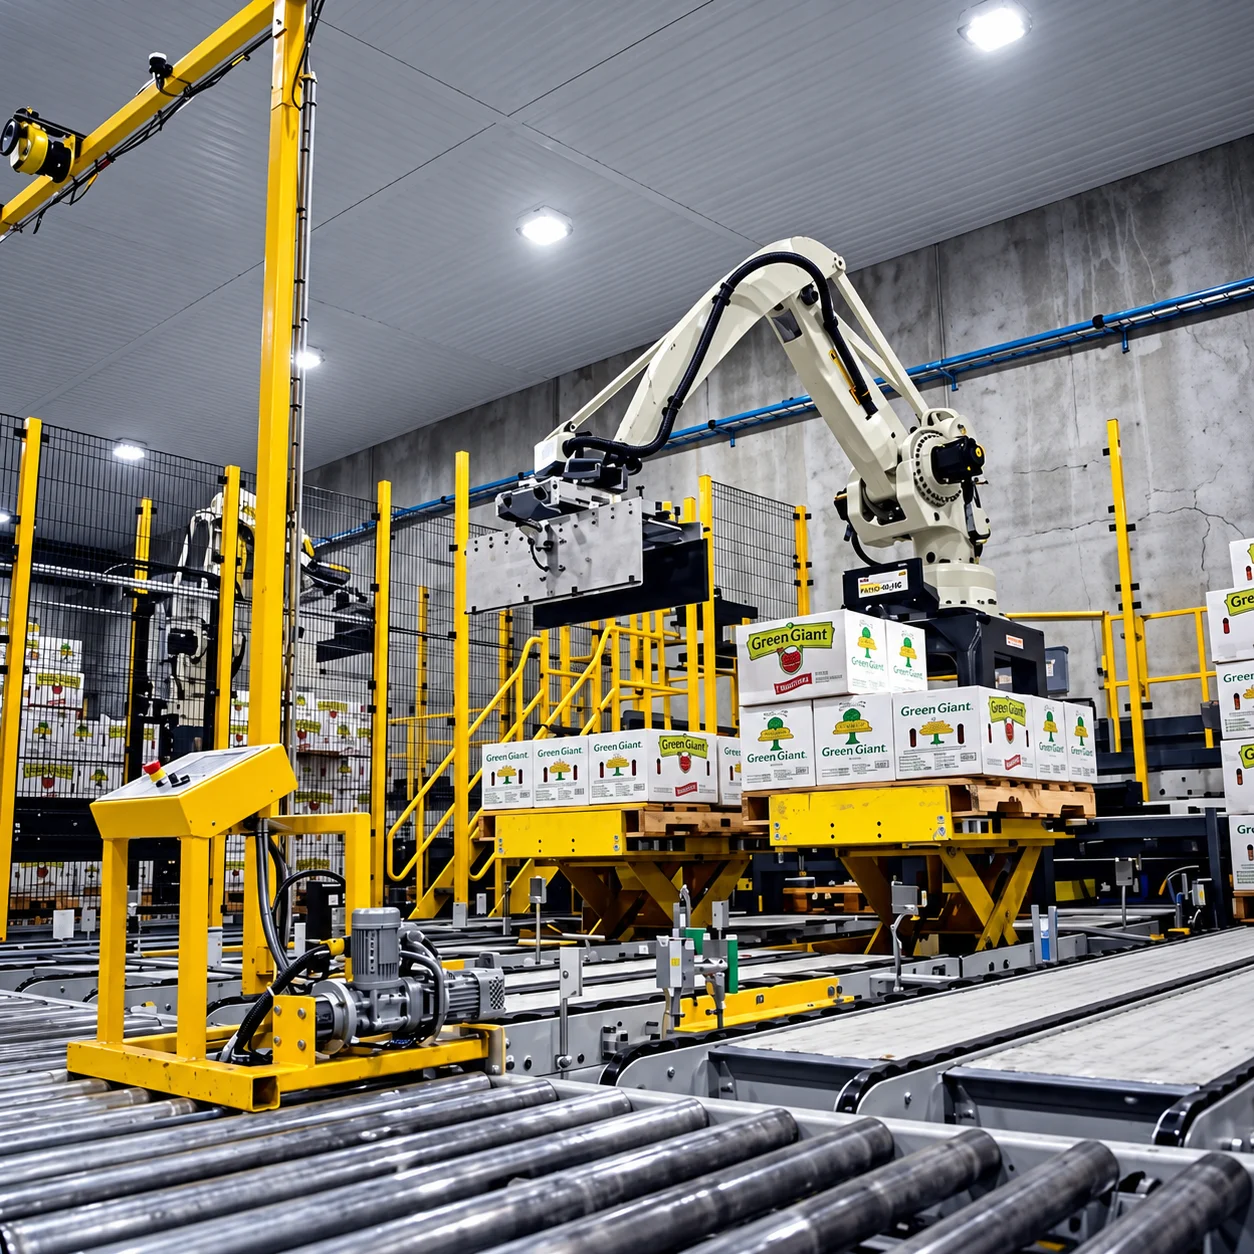
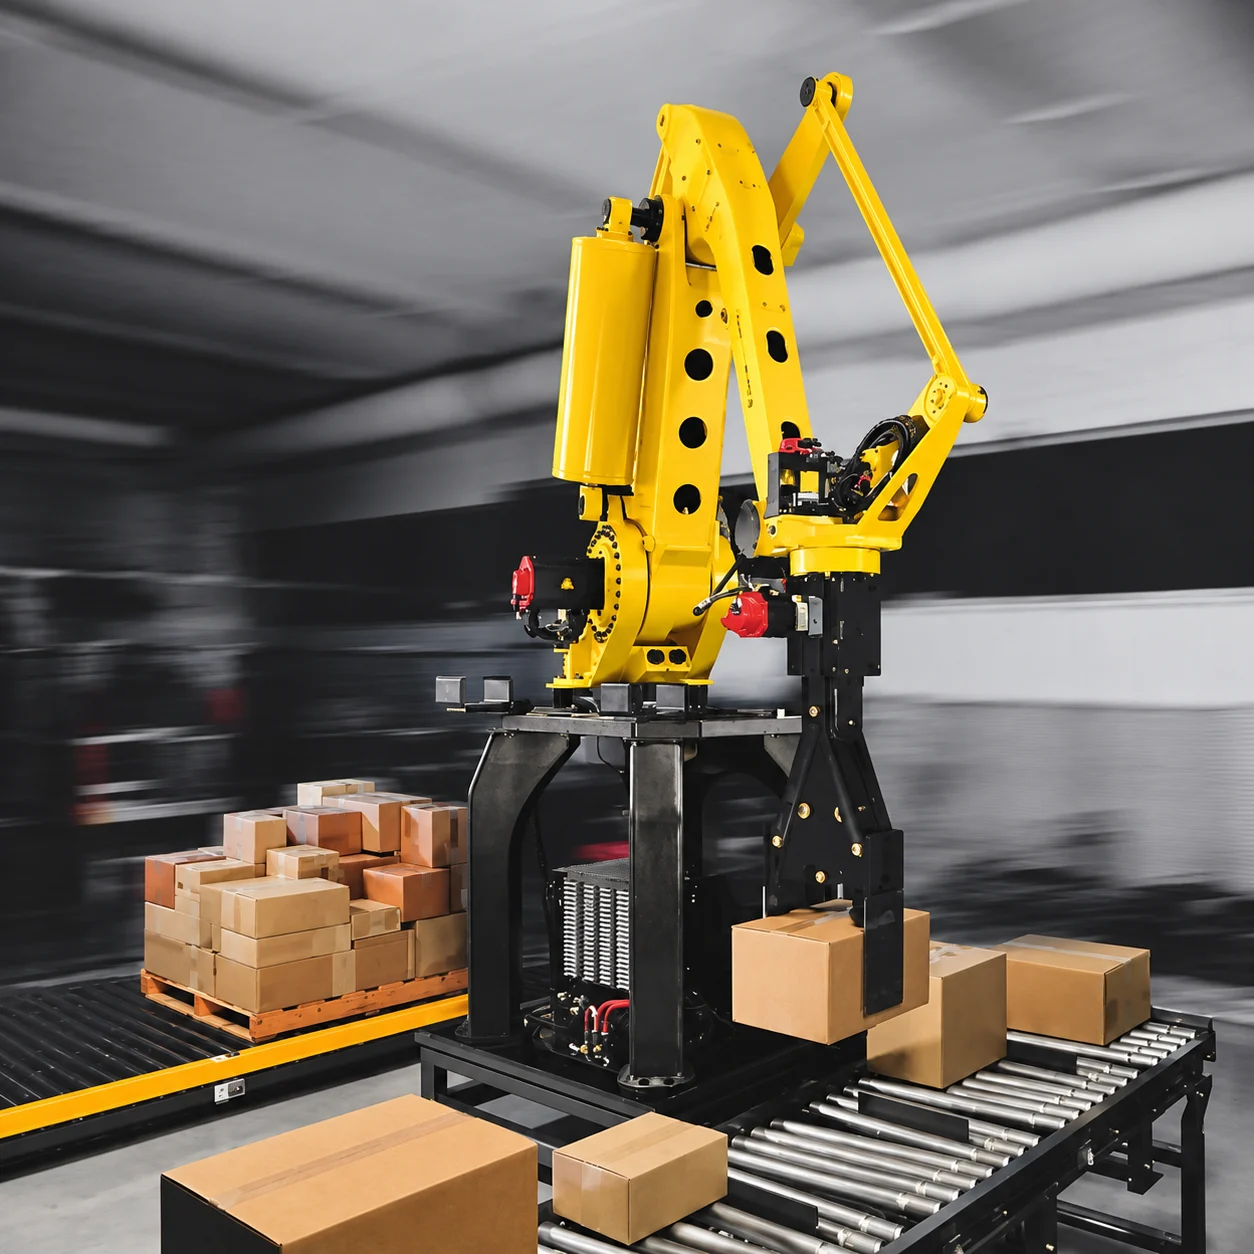
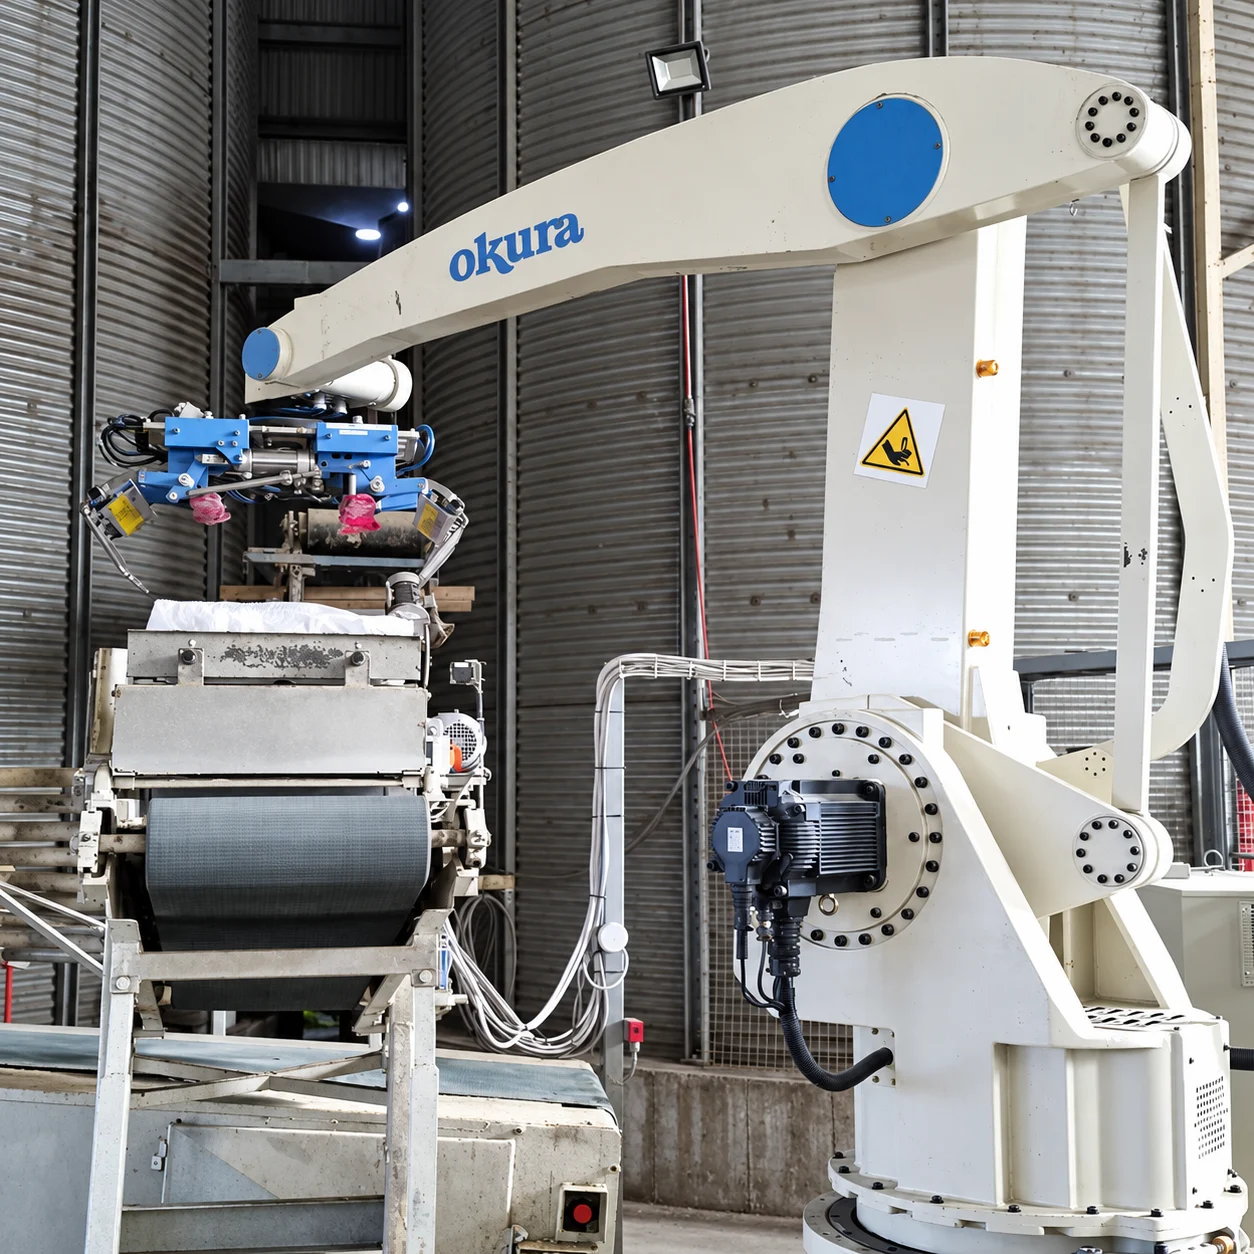
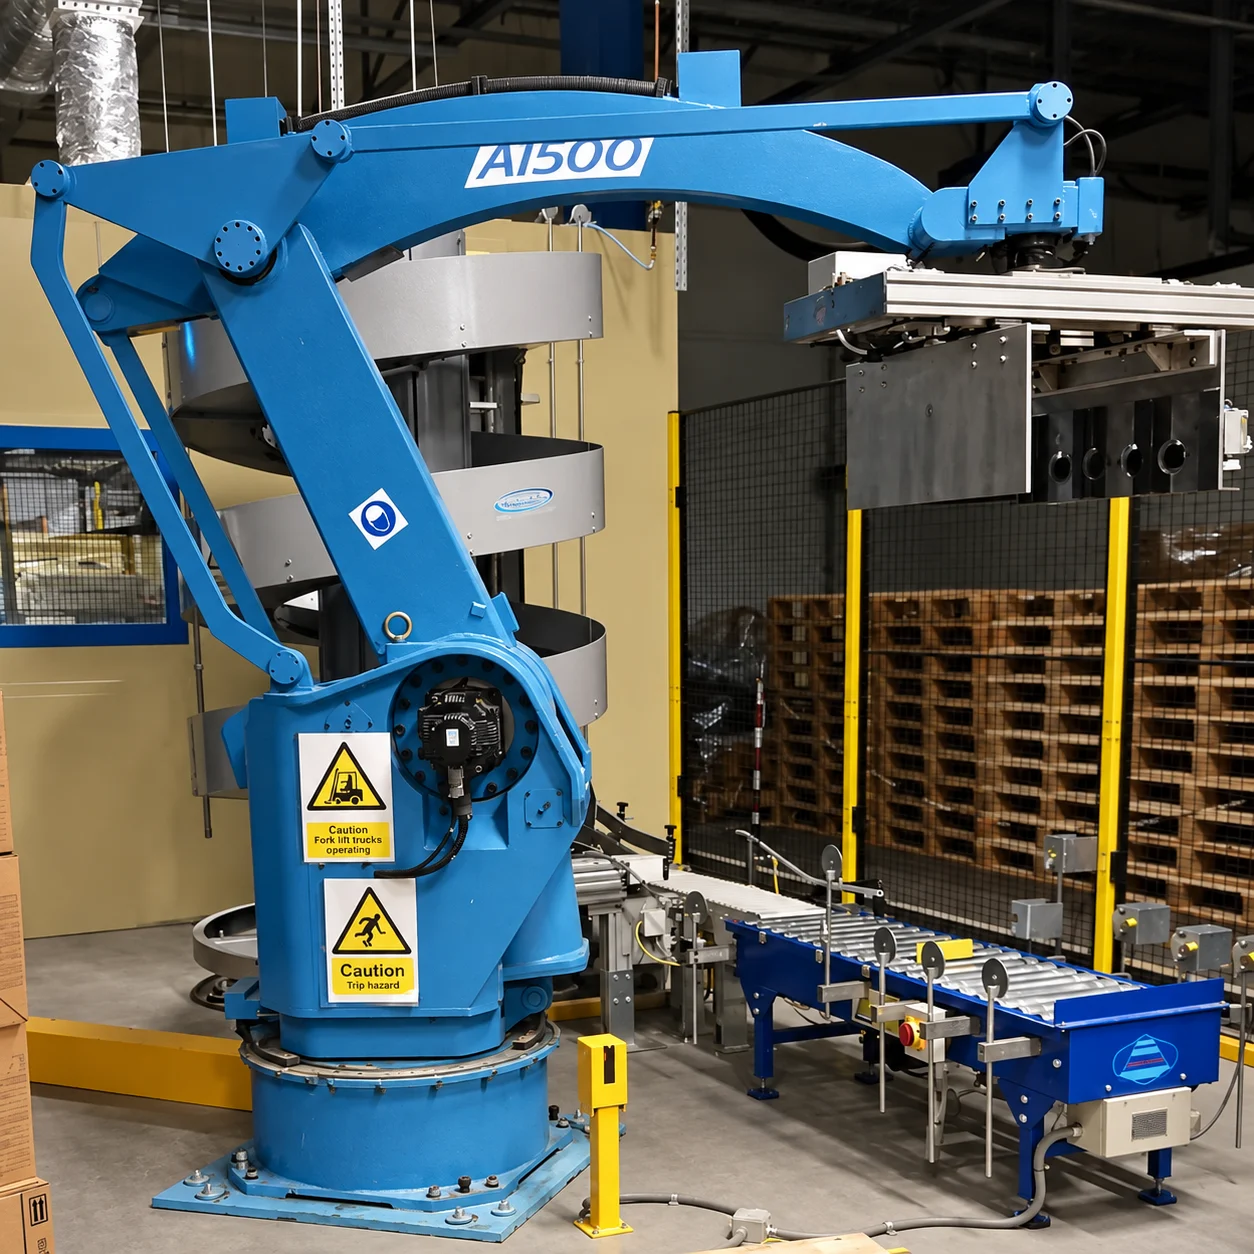
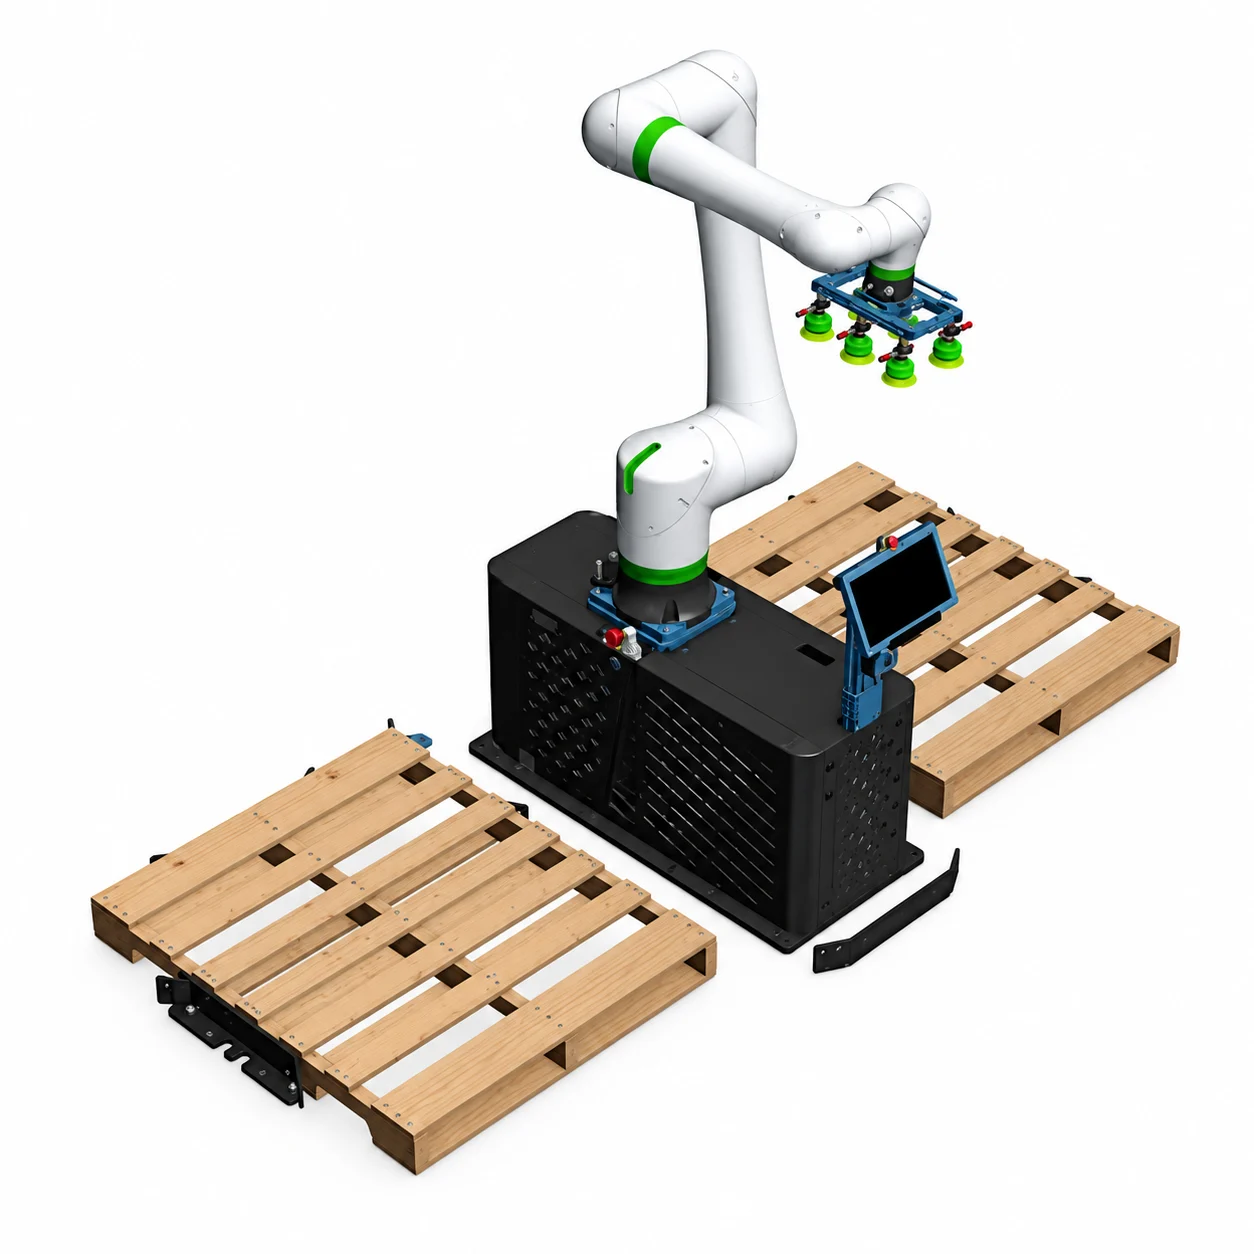
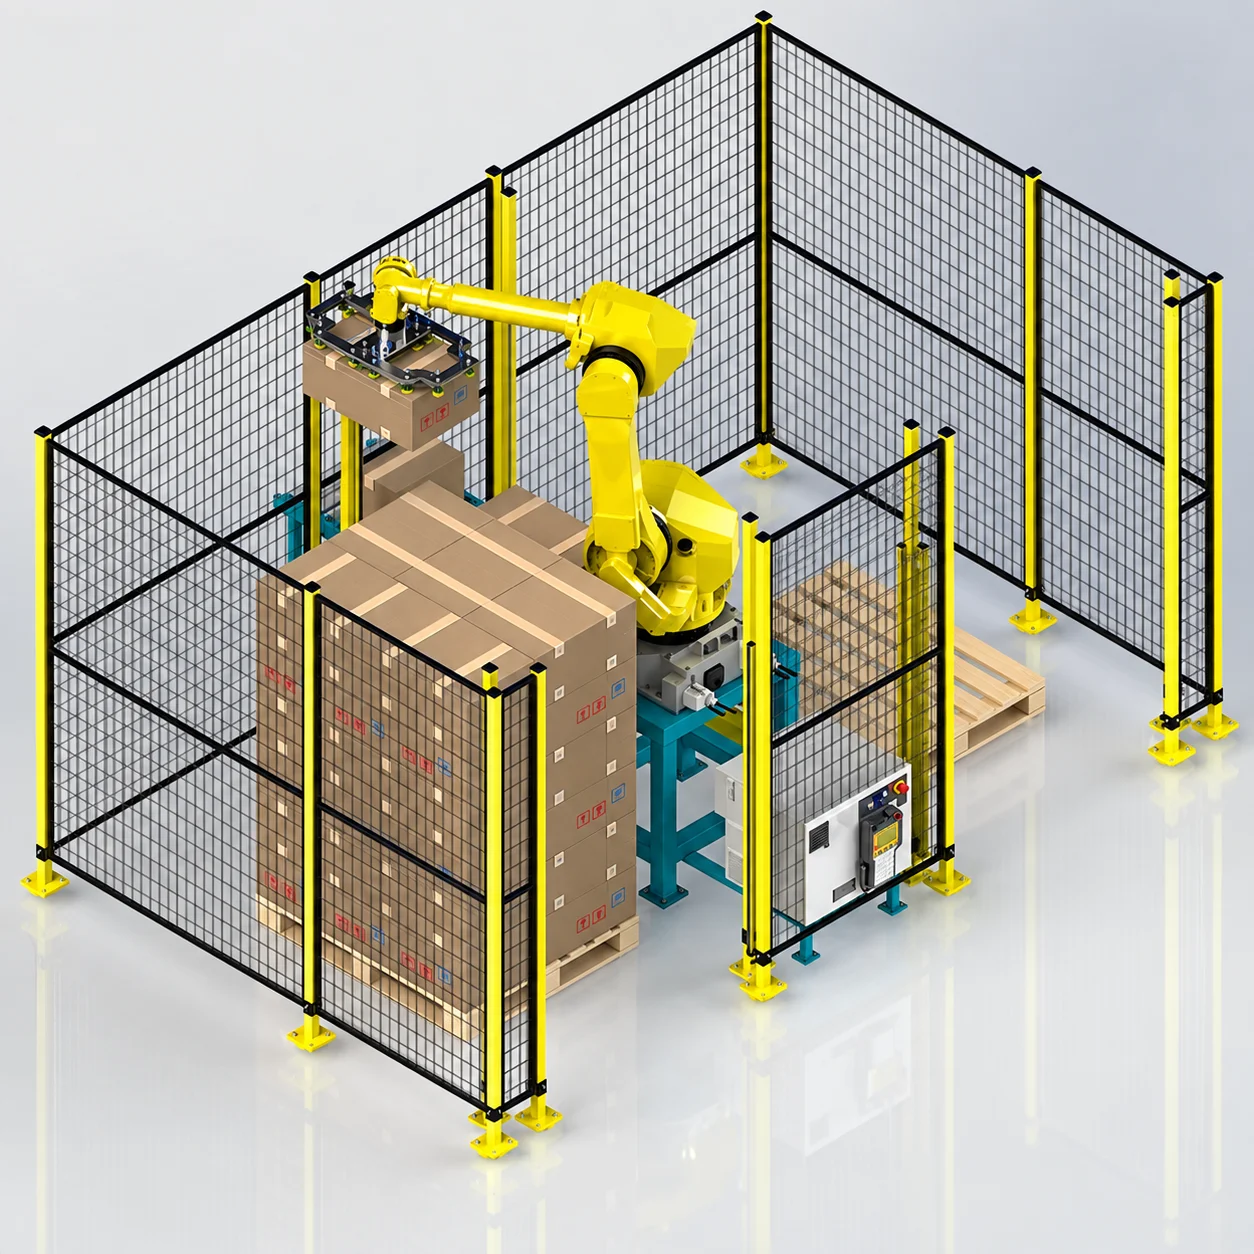
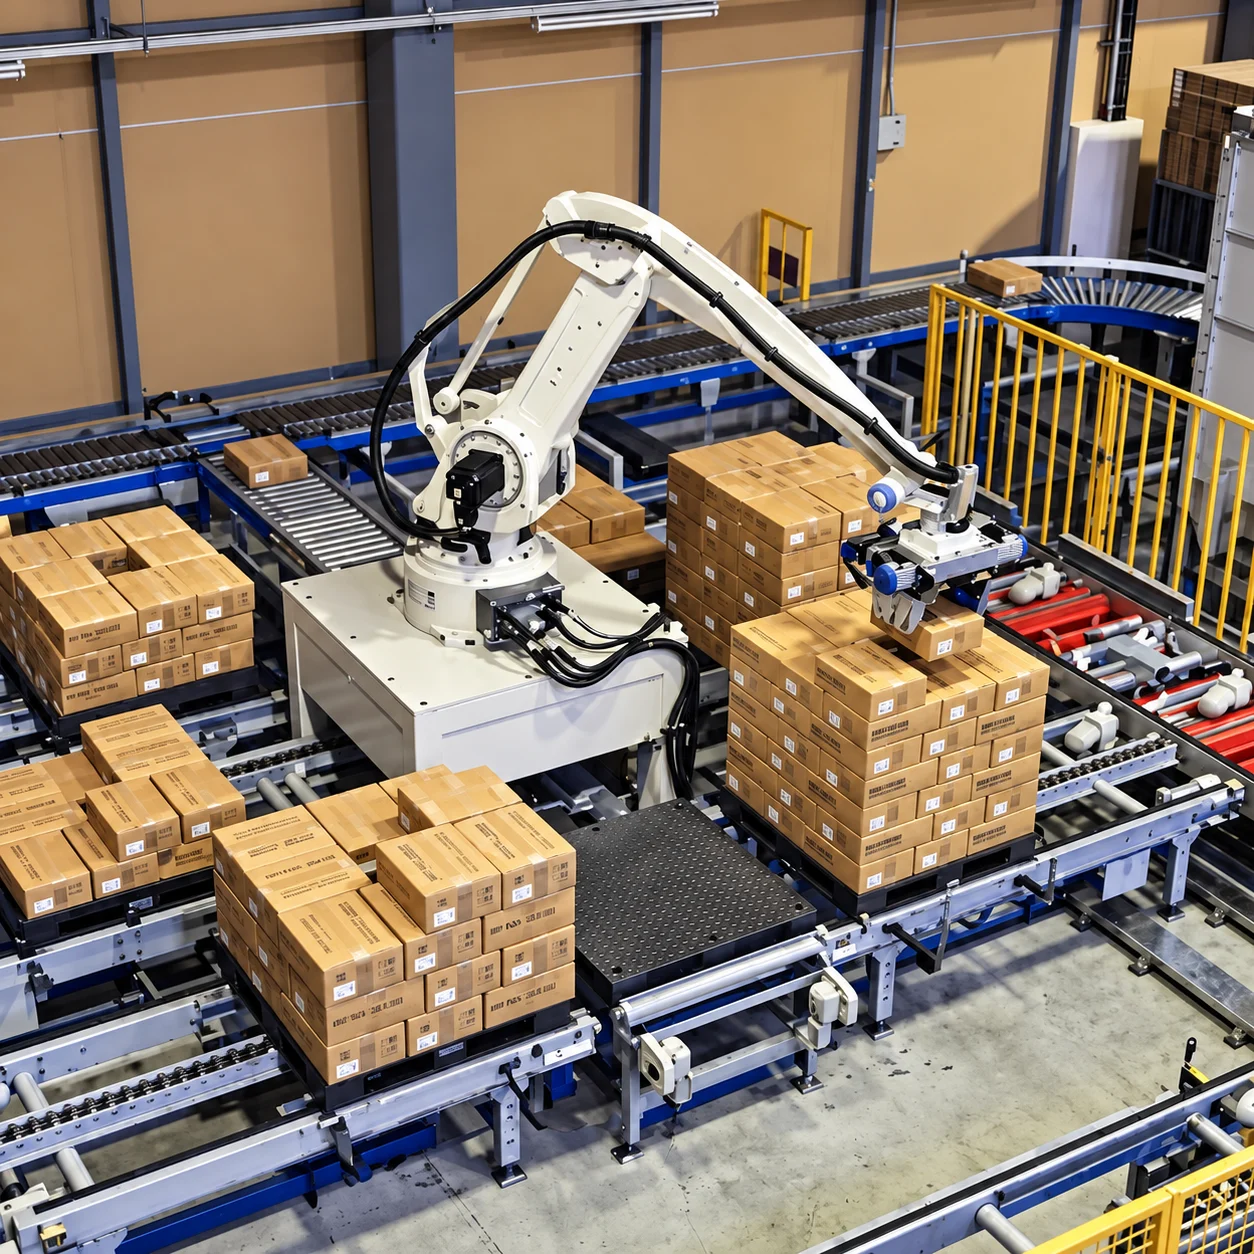
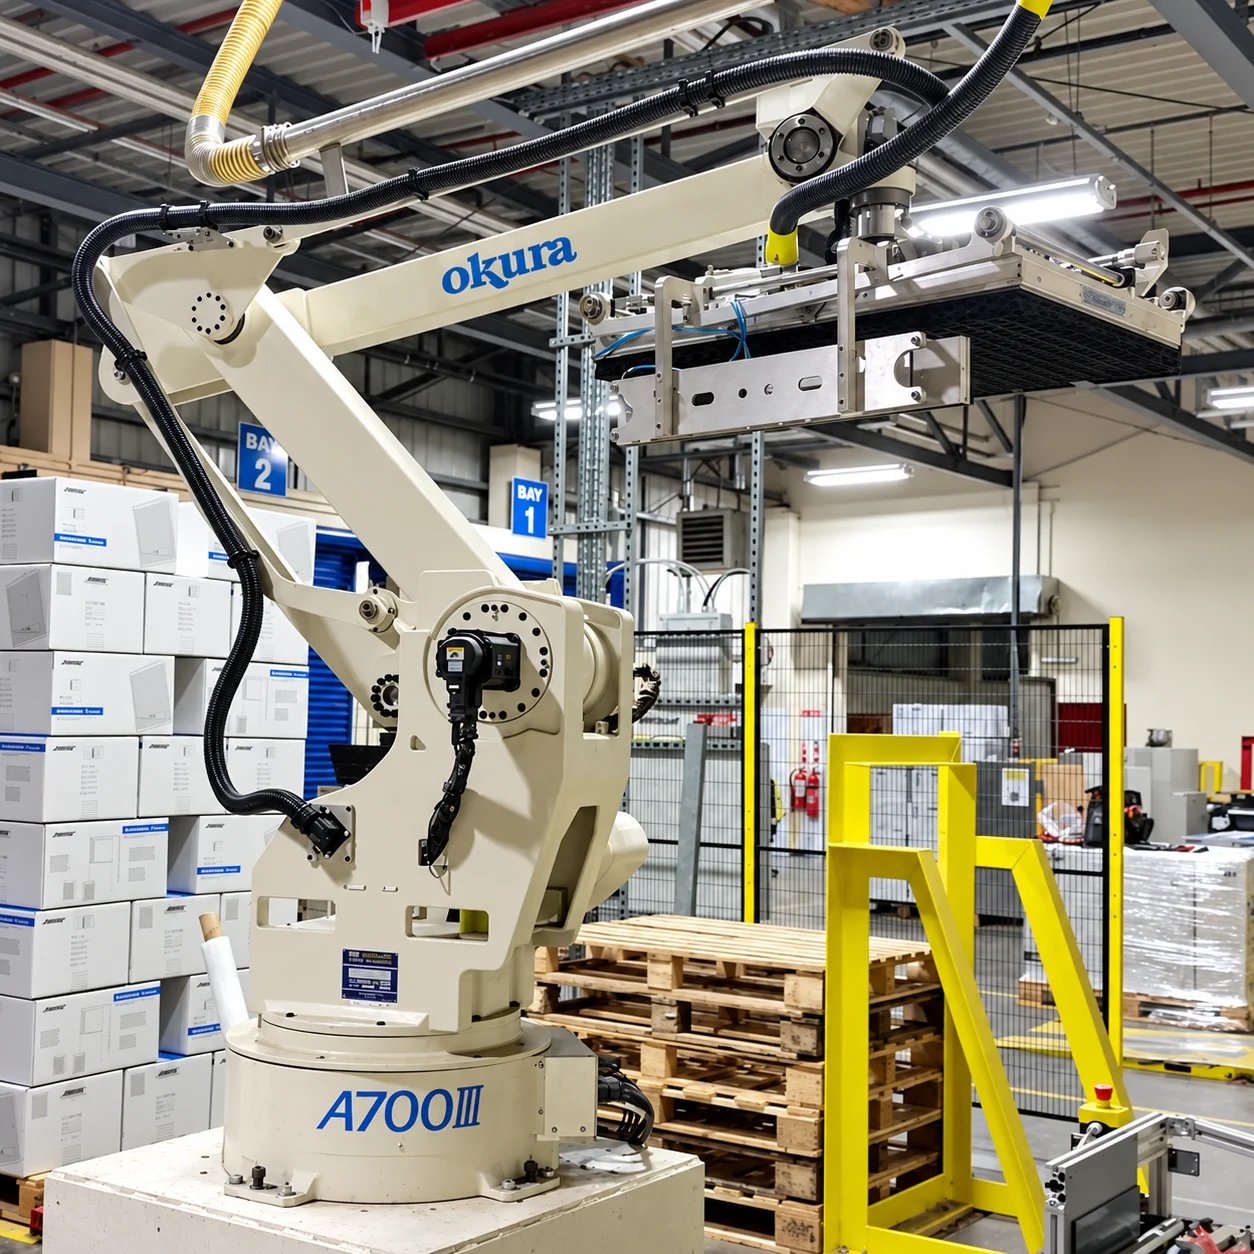
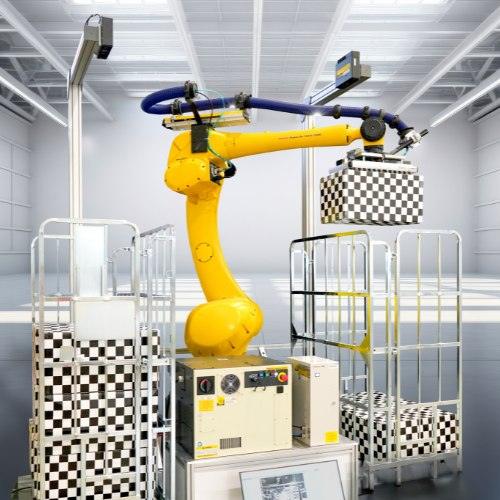
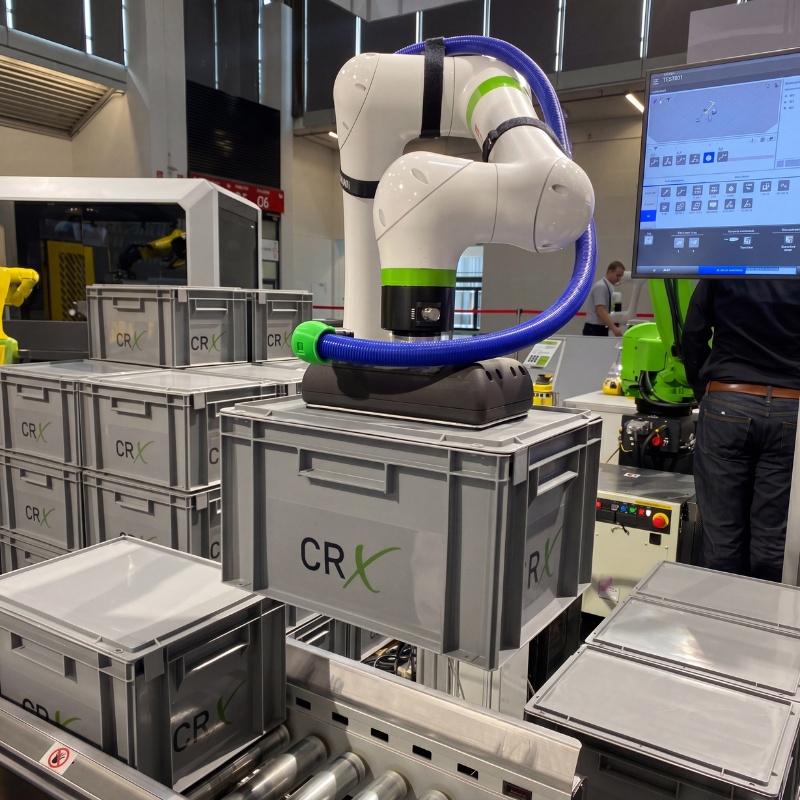
Robotic depalletisers that strip cartons, shrink wrapped trays, crates, totes and bagged goods off inbound pallets. Vision and 3D height mapping handle mixed SKU and imperfect stacks without precise patterns, at 8 to 20 picks a minute on single pick tooling. LVP Automation supply robotic depalletising cells built around Okura and Fanuc robots depending on the application.
Cell sized to your target throughputLayout, and simulation where it is warranted
Robotic depalletising explained
Why depalletising is the harder half of the job
Palletising is a known problem: the robot decides where every case goes, so it knows where every case is. Depalletising is the reverse, and the robot has to work out what arrived. Pallets come in from suppliers built to someone else's standard, leaning, shrink wrapped, with voids, crushed corners and layers that do not match the paperwork. That is why a depalletising cell leans much harder on sensing than a palletiser does, and why the vision specification matters more here than almost anywhere else on the line.
01
The Okura A Series, and what the models differ on
The Okura A Series is a four axis, multi articulated polar coordinate robot in four versions. The A700V, A1600V and A1800V all carry 140 kg; the A1800V-W carries 350 kg for heavy cases and full layer tooling. Working envelope is the same across the range apart from the vertical: D-axis 2,300 mm, T-axis 440 degrees and full 360 degree R-axis rotation, with O-axis 1,518 mm on the A1600V and A1800V and 1,750 mm on the A700V. That 360 degree rotation is what lets one robot serve up to six pallet positions from a single base, which is usually the difference between one cell and two.
02
Mixed SKU and rainbow pallets
Vision and pattern software identify each case and coordinate the pick order, so mixed case and rainbow pallets are a core strength rather than an exception. This is the clearest dividing line against conventional layer depalletisers, which need a uniform layer to lift. If your inbound pallets are single SKU and consistently built, a layer system may still be the cheaper answer. If they are not, and most distribution centre receiving is not, a robot with vision is doing something a mechanical system cannot do at any price.
03
8 to 20 picks a minute, and what moves that number
Okura rate the robots at 700 cycles an hour for the A700V, 1,600 for the A1600V, 1,800 for the A1800V and 500 for the heavy payload A1800V-W, and they are explicit that the handling rate depends on layout and on the hand, and that maximum payload is not the same thing as capacity. In a real depalletising cell, single pick rates typically land at 8 to 20 picks a minute depending on case weight, grip and travel path, with multi pick or layer tools going higher. Both numbers are useful: the first tells you what the arm can do, the second tells you what your cell will do. A shorter path is worth more than a faster robot, so bring a target throughput rather than a model number to the sizing conversation.
04
Grippers for cartons, trays, crates and bags
Loads handled include cartons, shrink wrapped trays, crates and totes, and many bagged goods. Gripper options run from vacuum with foam or cups, through clamp and fork or blade designs, to hybrids that combine two principles, plus dedicated slip sheet and pallet pick tools. Surface, porosity and stiffness decide which one works: a vacuum tool that holds a laminated carton will not hold an unlined kraft case, and a sagging bag needs support underneath rather than suction on top. This is the part to prove with real samples before anything is ordered.
05
Vision, height mapping and imperfect stacks
Precise pallet patterns are not required. Three dimensional height mapping tolerates misalignment, voids and deformed layers, and the cell adapts to stacks that are not perfect. Two dimensional vision handles case find and de-tiering, and barcode verification can confirm what has actually been picked against what the system expected. On inbound goods that check is worth having, because a receiving error found at the pallet is far cheaper than one found in the pick face.
06
Damage is a settings problem, not a robot problem
Product damage comes down to controlled acceleration, correct grip force and verified set-down locations, all guided by vision and safe trajectories. That is worth saying plainly because the instinct when throughput disappoints is to raise speed, and on a depalletiser that is usually how crushing and dropped cases start. The cell is tuned once around the weakest packaging you run, not the strongest, and throughput is found by shortening paths and improving presentation rather than by turning everything up.
07
Empty pallets, slip sheets and what happens downstream
A depalletising cell has to deal with more than cases. Slip sheet removal, empty pallet stacking and pallet infeed and outfeed all take floor space and all need deciding early, because they set the footprint as much as the robot does. Once the cases are off, they go onto conveyor for inspection, scanning and put-away. Getting that handover right is what keeps the cell running: a robot that can lift 20 cases a minute into a lane that only clears 12 is a 12 case a minute cell with an expensive arm on the front.
Footprint, integration and upkeep
Compact cells are possible, and the footprint depends on pallet infeed and outfeed, slip sheet stations and conveyor layout, so a layout drawing and, where it is warranted, a simulation come before any commitment. On Okura cells the Gen V controller carries the OXPA palletising software on an 8.4 inch touch screen, so stacking programs, product dimensions, layer counts and patterns are edited on the machine rather than through a programming pendant, and an integrated SICK safety PLC handles emergency stops, door switches and light guards. Integration is by PLC and HMI with network comms, and the cell can send SKU and quantity confirmations, faults and cycle data back to your WMS or ERP. Changeover is recipe or SKU selection at the HMI, with most format changes needing no reprogramming. Maintenance is routine checks on gripper seals, pads, filters and wear parts, scheduled robot servicing, and keeping vision lenses clean. The same robots also cover palletising, pick and place and machine tending. LVP Automation specifies, installs and supports robotic depalletising cells from Finglas, Dublin 11 as part of our wider automation services.
Specification
Okura A Series models
A700V, A1600V, A1800V and A1800V-W, all 4 axis multi-articulated polar coordinate
Maximum payload
140 kg on A700V, A1600V and A1800V; 350 kg on A1800V-W
Robot handling rate
700 cycles/hr A700V, 1,600 A1600V, 1,800 A1800V, 500 A1800V-W, subject to layout and hand
Cell pick rate
Typically 8 to 20 picks a minute on single pick tooling, higher with multi pick or layer tools
Reach and rotation
D-axis 2,300 mm, O-axis 1,518 mm (1,750 mm on A700V), R-axis 360 degrees, T-axis 440 degrees
Loads handled
Cartons, shrink wrapped trays, crates, totes and many bagged goods
Pallet types
Single SKU and mixed SKU rainbow pallets, including misaligned or deformed stacks
Vision
2D and 3D vision for case find, height mapping and de-tiering
Gripper types
Vacuum with foam or cups, clamp, fork or blade and hybrid, plus slip sheet and pallet pick tools
Controller
Okura Gen V with built-in OXPA palletising software, 8.4 in touch screen and integrated SICK safety PLC
Where Robotic Depalletising Excels
When to Choose Robotic Depalletising
Ideal for high inbound volumes, frequent SKU changes, irregular stacks and labour-constrained shifts. Reduces manual handling risk while keeping receiving lanes moving.
Vision, Tooling and Software
2D/3D vision for case find, height map and de-tiering; vacuum, clamp or fork grippers; slip-sheet handling; teach-free pattern changes and recipe selection at the HMI.
Typical Applications
DC receiving, cross-dock, goods-in for FMCG, food and beverage, pharma/medical and e-commerce, single or multi-line cells feeding conveyors, inspection and put-away.
FAQs about the Industrial Robot Depalletiser
Quick answers on products, patterns, vision, rates, changeovers, safety and integration.
What products can a robotic depalletiser handle?
Cartons, shrink-wrapped trays, crates/totes and many bagged goods. We choose grippers and vision to match surfaces, porosity and stiffness.
Can it process mixed-SKU or ‘rainbow’ pallets?
Yes, vision and pattern software identify each case and coordinate pick order. Mixed-case is a core strength versus conventional layer systems.
Do I need precise pallet patterns?
No. 3D height mapping tolerates misalignments, voids and deformed layers; the cell adapts to non-perfect stacks.
How fast can it run?
Typical single-pick rates are 8–20 picks/min depending on weight, grip and path; multi-pick/layer tools go higher. We size the cell to your target throughput.
How are changeovers handled?
Operators select a recipe/SKU from the HMI. With adaptable software, most format changes require no reprogramming.
What gripper types are available?
Vacuum (with foam or cups), clamp, fork/blade and hybrid designs; plus slip-sheet and pallet pick tools.
How does the system reduce product damage?
Controlled acceleration, correct grip force and verified set-down locations, guided by vision and safe trajectories.
What floor space is required?
Compact cells are possible; footprint depends on pallet infeed/outfeed, slip-sheet stations and conveyor layout. We provide a layout and (if needed) a simulation.
How does it integrate with my WMS/ERP?
Via PLC/HMI and network comms. The cell can send confirmations (SKU/quantity), faults and cycle data; scanners/vision can validate barcodes.
What maintenance is needed?
Routine checks on gripper seals/pads, filters and wear parts; scheduled robot service per OEM; vision lens cleaning and sensor health checks.
Have a question about our conveyor systems or need a tailored automation solution for your business? Our team at LVP Automation is here to help. Fill out the form below with your details, and we’ll get back to you as soon as possible. Whether you need a quote, technical support, or more information on our products, we’re ready to assist.